Industry Watch: The 4 Defects Customers Complain About Most—and Why They Keep Coming Back
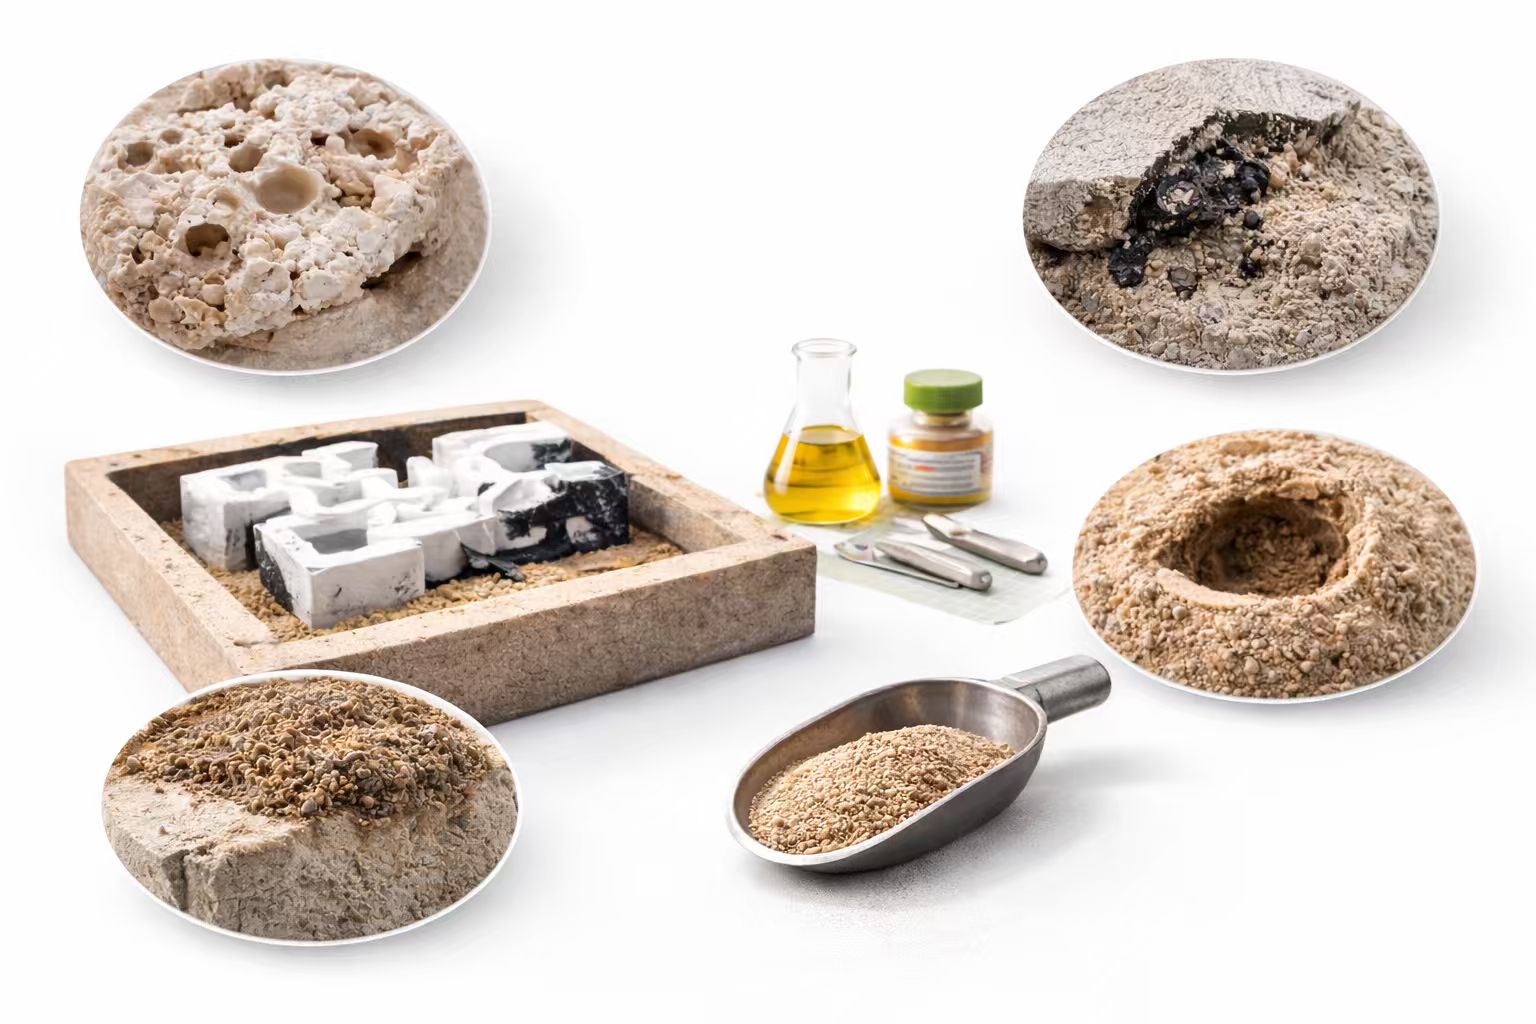
1) Gas Porosity: “The Part Looks Fine… Until Machining”
How it shows up
-
Pinholes and dispersed pores under the surface
-
Leaks in pressure testing
-
Machining reveals blowholes that were invisible in X-ray sampling
-
In aluminum especially: porosity “clusters” near thicker sections or junctions
What usually drives it
-
Hydrogen pickup (common in aluminum alloys) from moist charge, fluxing issues, poor degassing discipline
-
Turbulent filling that entrains air/oxide films (especially in aluminum)
-
Mold/core gas generation exceeding venting capacity (binder breakdown, high LOI materials, poor core bake, inadequate vent paths)
-
Temperature window drift: pouring too hot or too cold can worsen gas behavior depending on alloy/system
What the best-run shops emphasize
-
Stability first: fixed charge rules, controlled melt time, documented degassing cycles, and measured results (not “experience-based” only)
-
Venting as a design feature: not an afterthought—core vents, parting vents, and gating designed to reduce turbulence
-
Moisture control: storage discipline for binders, sand, and charge; simple humidity checks can prevent expensive scrap
2) Slag / Oxide Inclusions: “Random, Ugly, and Hard to Predict”
How it shows up
-
Non-metallic streaks or “dirty” spots on fracture surfaces
-
Localized weak points, unexpected fatigue failures
-
Rejection spikes after a furnace lining change or scrap mix shift
-
In aluminum: oxide film defects can masquerade as porosity or cracks
What usually drives it
-
Dirty charge or inconsistent scrap preparation
-
Poor skimming practice (wrong timing or tool; disturbing the slag layer)
-
Re-oxidation during pouring from excessive turbulence, long pour height, or poor ladle practice
-
Temperature and holding effects: longer holding can increase oxidation or dross formation if not managed
What the best-run shops emphasize
-
Clean melt habits: charge preparation, furnace housekeeping, ladle discipline, and consistent skim timing
-
Flow control: calmer metal transfer and better gating to reduce surface turbulence
-
Root-cause logs: when inclusions rise, they trace it back to a specific change (scrap source, flux, ladle lining, operator shift, etc.)
3) Sand-Related Surface Defects: Burn-on, Penetration, and “Sticking”
How it shows up
-
Rough surface, fused sand patches, heavy cleaning and grinding
-
Local “burn-on” around hot spots or high-velocity areas
-
Mold erosion marks, veining, scabbing, or sand wash
-
Higher rework cost even if the casting passes dimensional checks
What usually drives it
-
Sand system instability: inconsistent grain distribution, excess fines, or sudden binder fluctuations
-
High metal temperature / long contact time at hot spots
-
Insufficient refractoriness or poor coating practice for the application
-
Gas + surface chemistry interactions: when gas can’t escape, it pushes defects to the surface (especially around cores)
What the best-run shops emphasize
-
Sand and binder control as a “process,” not a material: routine checks, documented adjustments, and clear acceptance ranges
-
Targeted coatings and localized solutions: they don’t “over-coat everything,” they coat where physics demands it
-
Design alignment: gating/runner design that avoids high-velocity impingement on mold surfaces
4) Shrinkage Defects: The Classic Problem That Still Wins
How it shows up
-
Centerline shrinkage, spongy zones, cavities at junctions
-
NDT reveals internal voids even when surface looks perfect
-
“Random” failures that correlate with section thickness changes
-
Repair welding becomes frequent—and expensive
What usually drives it
-
Feeding design mismatch: risers, chills, and feeding paths not aligned with solidification
-
Pouring variability: temperature drift and inconsistent fill time change solidification behavior
-
Alloy behavior + geometry: complex junctions, abrupt thickness changes, poor directional solidification
-
Over-correction: aggressive cooling fixes one defect but triggers another (e.g., cold shuts or misruns)
What the best-run shops emphasize
-
Directional solidification logic: they design the freeze pattern deliberately
-
Simulation + validation: not every shop can simulate everything, but leaders validate changes with disciplined trials
-
Process repeatability: shrinkage is very sensitive to “small shifts” that many plants tolerate
A Real-World Pattern: Why “Quick Fixes” Don’t Stick
A common scenario in resin-bonded or coated-sand operations:
-
A porosity spike appears → the plant increases venting and lowers binder →
-
Surface finish worsens or sand-related defects rise → they increase coating and adjust sand fineness →
-
Filling behavior changes → inclusions or shrinkage complaints rise →
-
The plant ends up chasing symptoms across departments.
The lesson isn’t that any one adjustment is wrong—it's that defects are interconnected. The best results come from treating quality as a system:
-
Melt cleanliness and transfer discipline
-
Controlled pouring practice
-
Sand system stability (grain distribution + binder consistency + gas management)
-
Gating/feeding design aligned with physics
-
Measurement and documentation that survive shift-to-shift variability
Practical Checklist: What to Review First When Scrap Rises
If your rejection rate increases and it’s not obvious why, start with these high-impact checks:
-
Melt: charge moisture, skimming timing, transfer turbulence, ladle cleanliness
-
Pouring: temperature window, pour height, fill time consistency, interruption events
-
Sand/Core: binder storage, LOI trends, core bake/cure consistency, vent routes
-
Design: gating impingement zones, riser effectiveness, hot spot locations
-
Discipline: “what changed recently?” (supplier, scrap mix, shift, equipment, coating, maintenance)
Outlook: Quality Wins Will Come From Stability, Not One-Time Upgrades
Most foundries can name the defect—they struggle with repeatable prevention. As customer standards tighten and rework costs climb, the competitive edge will increasingly come from:
-
stable sand and binder control,
-
disciplined melt cleanliness,
-
reduced turbulence and better gas management,
-
and process traceability that makes problems diagnosable in hours—not weeks.
That’s the difference between “fixing defects” and running a defect-resistant operation.
2024–2025 Global Foundry Industry Observation: Reshaping Capacity Structure and Material Selection Amid Fluctuations
Related Article