Technical Feature: How Sand Cores Are Made—and Where Fused Ceramsite Sand Adds Real Process Value
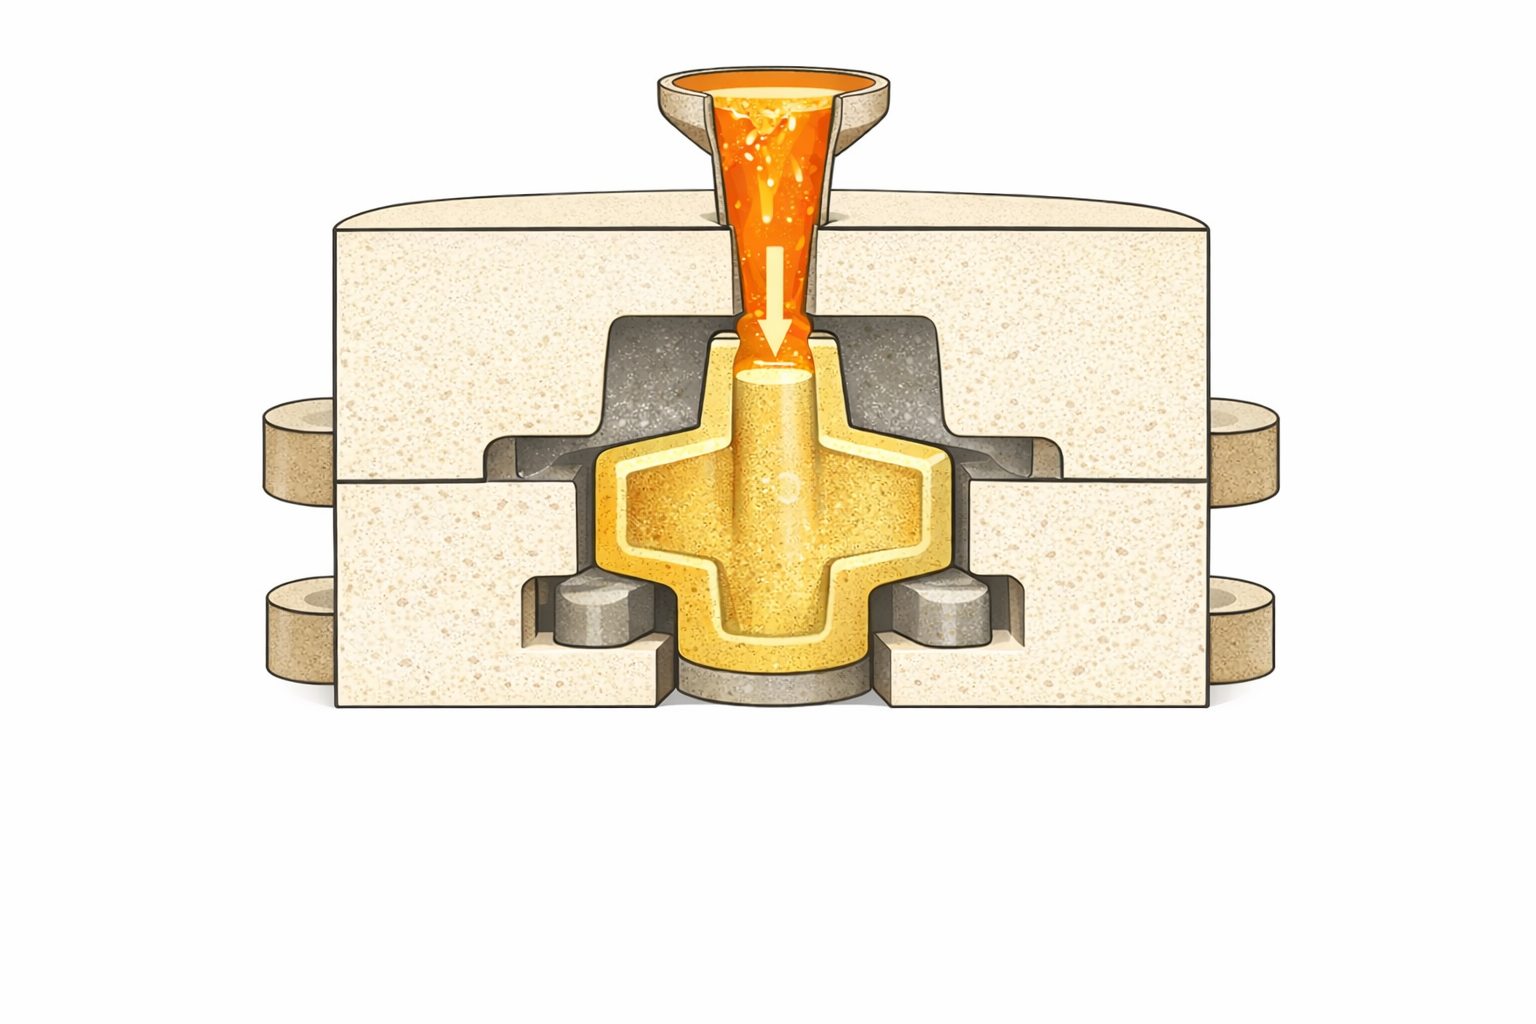
1) What a Sand Core Does (and Why It Fails So Often)
A sand core is a pre-formed sand body placed inside a mold to create internal features of the casting. During pouring, the core experiences:
-
Instant thermal shock and high heat flux
-
Metallostatic pressure and turbulent flow, especially near gates and runners
-
Gas generation from binders and additives
-
Mechanical vibration and handling loads prior to pouring
-
Chemical and physical interaction at the metal–core interface
Because cores sit “inside” the casting, a core issue is not always visible until machining, X-ray inspection, pressure testing, or end-of-line functional testing. That is why core-making consistency is not just a quality topic—it is a production risk topic.
2) How Sand Cores Are Made: Principle and End-to-End Workflow
At its most basic level, a core is made by mixing a granular media (sand) with a binder system, shaping it inside a core box, then curing it to build enough strength for handling and pouring. The details vary by process, but the structure of the workflow is similar across modern core rooms.
Step A: Media selection and grading design
Before binder is discussed, core performance is largely shaped by the base media:
-
Grain size and distribution (AFS/mesh, multi-peak grading, fines control)
-
Particle shape and packing behavior (flowability vs. strength vs. permeability)
-
Dust and ultra-fines (impacts viscosity, binder demand, and gas)
-
Thermal behavior (thermal expansion, heat conductivity, thermal shock)
-
Chemical purity and high-temperature stability (burn-on and sintering tendency)
A core mix that looks “fine” at room temperature can behave completely differently at pouring temperature. This is why media selection is a technical decision, not just a purchasing decision.
Step B: Mixing and coating (binder + additives)
The binder system depends on process type:
-
Cold box (amine gas-cured)
-
Hot box / warm box (thermally cured resin)
-
Shell core (resin-coated sand, hot-coated)
-
No-bake / self-setting systems
-
Inorganic binders (CO₂ / water-glass types and newer inorganic systems)
The objective of mixing is uniform distribution: every grain should receive a consistent binder film so the cured matrix has predictable strength and gas behavior. Poor distribution leads to “strong outside, weak inside” cores or inconsistent breakage.
Step C: Shooting or filling into the core box
This is where flowability becomes critical. In practice, core boxes contain thin walls, sharp corners, ribs, and varying section thickness. The media must fill these details without segregating.
Key variables here include:
-
Flowability and “shootability”
-
Packing density uniformity (local density drives local strength and permeability)
-
Venting effectiveness and trapped air paths
-
Tooling surface condition and temperature stability
Step D: Curing and strength development
Curing method determines how strength forms:
-
Gas curing (cold box): cure speed and penetration depth depend on permeability, compaction, venting, and chemistry
-
Thermal curing (hot box/shell): heat transfer depends on packing structure and media thermal properties
-
Inorganic systems: drying and moisture management dominate
The core must achieve handling strength quickly, but also maintain dimensional stability over storage and assembly.
Step E: Core removal, trimming, inspection, and coating (optional)
After ejection, operators remove flash, repair small damage, and may apply refractory coatings:
-
Coating improves surface finish and reduces metal penetration
-
Coating drying must be controlled to avoid moisture-related gas issues
-
The base media influences how coating wets and anchors on the surface
Step F: Storage, assembly, and pouring
Core quality can degrade during storage:
-
Humidity pickup and moisture-related strength loss
-
Mechanical damage during handling
-
Dimensional drift due to stress relaxation in long or thin cores
-
Surface contamination (dust, oil mist, shop residue)
A stable media choice reduces sensitivity to these environmental factors.
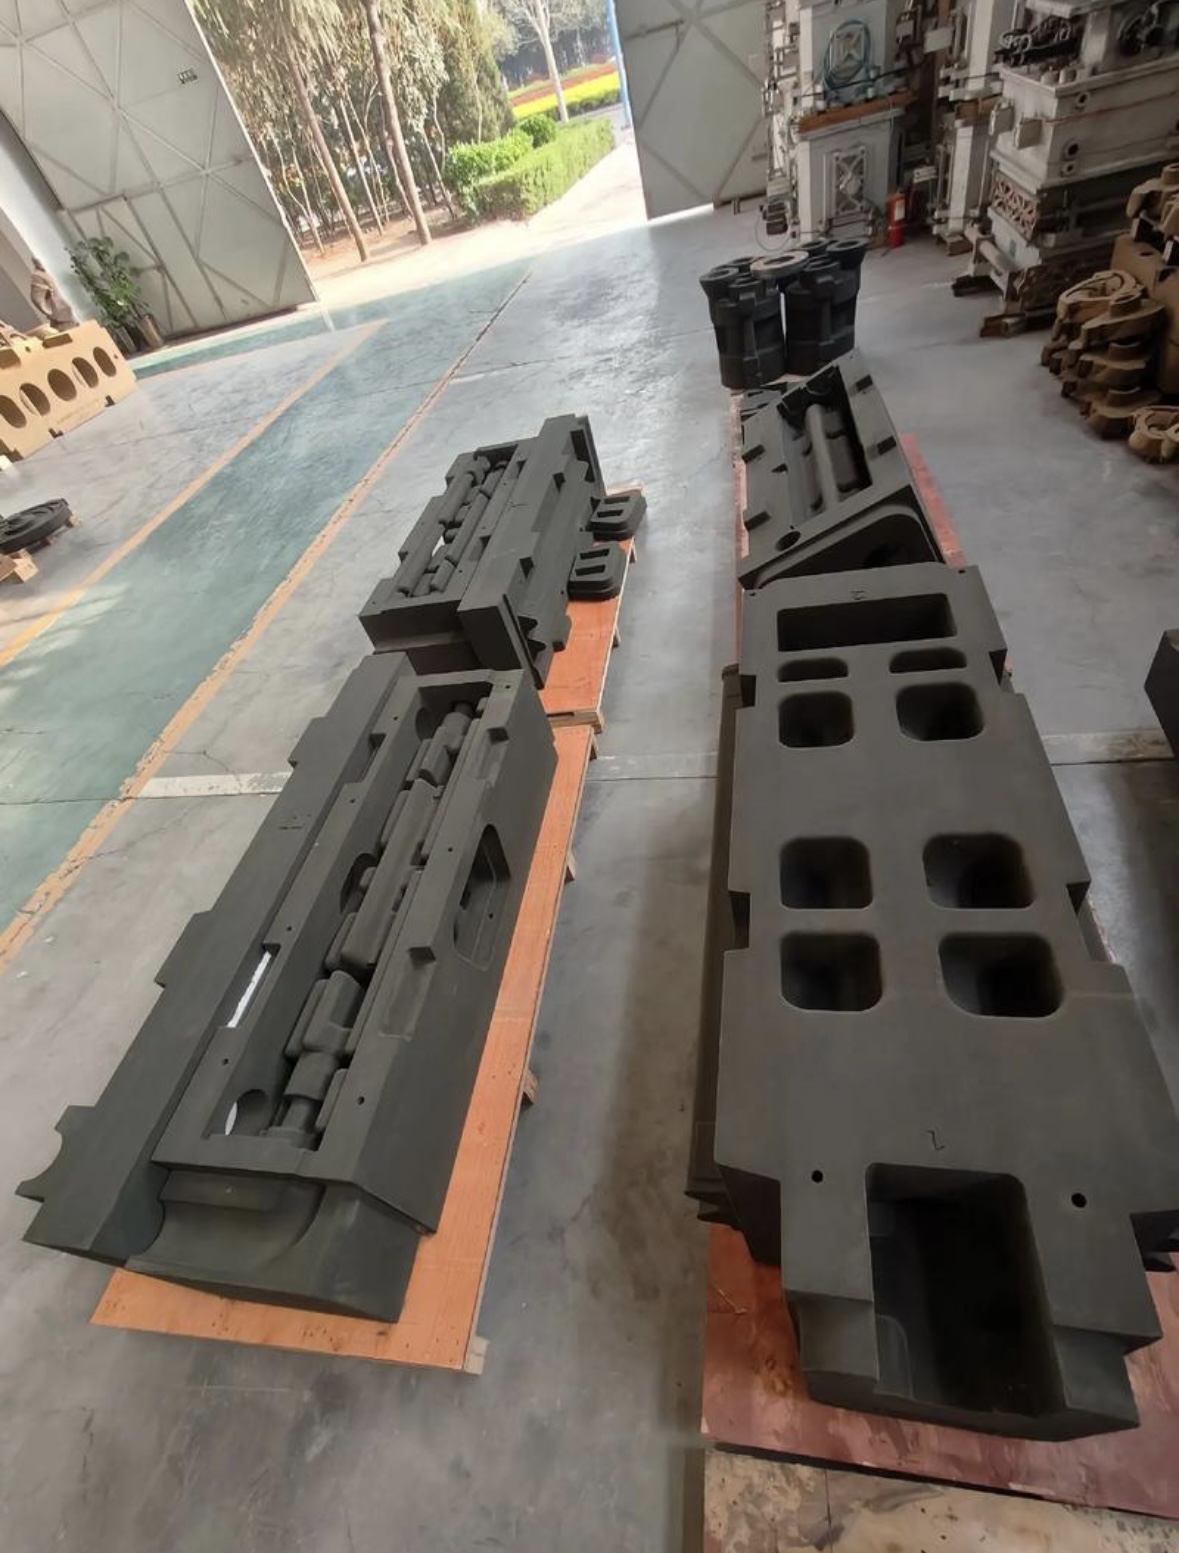
3) Common Sand Core Problems in Production—and Root Causes
Below are the most frequent core-related failures seen in real production, with core-making root causes that matter technically.
Problem 1: Gas defects (pinholes, porosity, blistering)
Typical symptoms:
-
Pinholes on internal surfaces
-
Porosity clusters near core prints or thick sections
-
Blistering at hot spots
Core-related causes:
-
High binder dosage or uneven binder distribution
-
Low permeability due to excessive fines or over-compaction
-
Moisture contamination (especially in inorganic or coated cores)
-
Poor venting design and trapped gas pockets
-
Slow curing zones that retain volatile species
Problem 2: Sand inclusion, erosion, and wash defects
Typical symptoms:
-
Sand inclusions inside the casting
-
Erosion lines near gates or high-velocity flow areas
-
Rough internal surfaces and local metal penetration
Core-related causes:
-
Low hot strength or weak surface layer
-
Poor compaction uniformity
-
Weak edges/corners caused by incomplete fill
-
Media that fractures into angular fragments under thermal shock
Problem 3: Burn-on, sintering, and difficult cleaning
Typical symptoms:
-
Strongly adhered sand on internal surfaces
-
Sintered layer that resists shakeout
-
Increased grinding and cleaning time
Core-related causes:
-
Chemical interaction between media impurities and metal oxides
-
Local overheating and metal penetration into the core surface
-
Media with poor refractoriness stability under high thermal load
-
Coating incompatibility with base media surface structure
Problem 4: Dimensional shift and internal geometry variation
Typical symptoms:
-
Internal channels off location
-
Machining mismatch or leak test failures
-
Variation batch-to-batch despite stable tooling
Core-related causes:
-
Media thermal expansion and thermal shock response
-
Uneven compaction causing uneven thermal deformation
-
Cure-induced internal stresses in long/thin cores
-
Inconsistent grading or fines content leading to different packing behavior
Problem 5: Core cracking, breakage, and handling damage
Typical symptoms:
-
Cracked cores on ejection or during assembly
-
Edge breakage and chipping
-
Core print damage
Core-related causes:
-
Local weak zones from poor flowability or segregation
-
Binder film not uniform
-
Overbrittle cured matrix (excess binder or wrong cure profile)
-
Media particle shape creating stress concentrations
Problem 6: Poor collapsibility (hard shakeout, trapped core)
Typical symptoms:
-
Core remains hard after pouring
-
High labor time for internal cleaning
-
Risk of casting damage during shakeout
Core-related causes:
-
Over-strong matrix at pouring temperature
-
Media that sinters and locks together
-
Binder system and media interaction that produces high residual strength
4) Where Fused Ceramsite Sand Helps: Mechanisms That Matter in Core Rooms
Fused ceramsite sand is an engineered ceramic media. In core-making, its value is best understood as “process stability leverage.” It does not replace good core design, venting, or binder control—but it can reduce sensitivity to variables that cause drift.
4.1 Flowability and fill completeness in complex core boxes
In real core shops, the hardest geometry is not the large cavity—it is the thin ribs, corners, and long internal passages. Media stability supports:
-
More consistent fill in thin sections
-
Reduced risk of unfilled corners and weak edges
-
Less segregation during shooting, supporting uniform density
When density is uniform, strength and permeability are more predictable across the entire core.
4.2 Balanced permeability and strength
Core rooms constantly trade off permeability and strength. Too dense and gassy, too open and weak. A media with stable grading and controlled fines enables a more repeatable “window”:
-
More stable gas escape paths
-
Reduced need to increase binder just to hit strength targets
-
Lower risk of gas defects caused by over-binder solutions
4.3 Thermal stability: controlling thermal expansion-driven variation
Internal dimensional accuracy depends on how the core behaves at high temperature. Lower expansion and stable thermal response can help reduce:
-
Thermal expansion-related internal shifts
-
Crack initiation from thermal stress
-
Variability across pours, especially for long thin cores
This is particularly relevant when the casting has narrow internal tolerances or leak-critical passages.
4.4 Surface integrity and reduced metal penetration
Even when coatings are used, the base media affects how the surface behaves under turbulence and pressure:
-
Improved resistance to erosion when hot strength is stable
-
Reduced tendency toward local breakdown at gates or near hot spots
-
More stable internal surface finish, reducing downstream cleaning time
4.5 Cleaner process control: reducing batch-to-batch drift
Many core defects come from drift rather than “one-off mistakes.” Media consistency helps reduce:
-
Variation in mixing torque and binder demand
-
Variation in curing behavior (gas penetration, heat transfer)
-
Variation due to seasonal humidity effects and dust buildup
In a production environment, less drift means fewer parameter changes and fewer “mystery defects.”
5) Practical Guidance: How Core Shops Evaluate Media Changes
When a foundry or core shop considers a media shift, the best approach is to treat it as a structured validation, not a trial-and-error exercise. A typical evaluation checklist includes:
-
Core strength curve
-
Immediate handling strength and 24-hour strength
-
Hot strength proxy tests when available
-
Permeability and gas behavior
-
Measured permeability at representative compaction
-
Gas evolution testing if internal porosity is a known issue
-
Dimensional repeatability
-
Gauge critical internal features across multiple shifts and batches
-
Include storage time impact (same-day vs. next-day assembly)
-
Surface and cleaning effort
-
Compare internal surface finish
-
Track shakeout time and internal cleaning hours
-
Defect mapping
-
Before/after defect Pareto for inclusion, porosity, burn-on
-
Tie defect changes back to measurable core parameters
This is the fastest way to determine whether improvements are real, repeatable, and scalable.
6) Summary: A Technical View of “Why Media Choice Changes Core Outcomes”
Sand core performance is not determined by binder alone. The media defines the core’s packing structure, permeability pathways, thermal response, and the stability of the curing environment. Once pouring begins, these properties govern whether gases escape, whether the surface holds, and whether internal dimensions remain consistent.
Fused ceramsite sand is valuable in core-making because it can improve process repeatability across mixing, shooting, curing, storage, and pouring—reducing the sensitivity that often drives defects and rework in modern casting operations. In a world of higher complexity castings, thinner walls, tighter internal tolerances, and stronger cost pressure, stability is not a luxury; it is a competitive requirement.
Process Matters: Why Lost Foam Casting (EPC/LFC) Demands a Different “Sand System”
Related Article